
10 min read
Laser cutting
→Sheet metal finishing after cutting: deburr or leave
Choose the edge finish after cutting by what happens next: coat, weld, slide or show. Ra values, edge radius, method and the minutes each one adds.
Ganesh engineering library
377 guides on stamping, laser cutting, bending, welding, coating and the parts we build for lift, power, data centre, railway and farm equipment. Every article is reviewed by the engineering team before it is published.
Nine clusters, each mapped to a capability or product page.
Choose the edge finish after cutting by what happens next: coat, weld, slide or show. Ra values, edge radius, method and the minutes each one adds.
Bend allowance is the arc through the neutral axis: 3 mm CRCA at R3 and 90° gives 6.79 mm, a 5.21 mm deduction and a 324.79 mm flat. Formula, table and worked steps.
Forklift counterweight cover design: clearance to the casting, panel stiffness, hinge geometry, coating and inspection limits for a 1.5 mm CRCA shroud.
Forklift guard impact design: the 662 J drop, roof bar hinge arithmetic, the failures that appear after the test and the drawing fields that prevent them.
ISO 12944 corrosion protection explained: corrosivity categories C1 to CX, the film build each needs, durability classes, and why sheet-metal enclosures differ.
A material or process change leaves the drawing untouched and moves the part. What a first article must measure when the revision never changes.
A hole near a bend fails in two ways: it goes oval from the strain gradient and it lands off position from the flat pattern. How to separate and prevent both.
How an elevator pit ladder is cut, welded and powder coated, with rung load, pitch, clearance and anchor numbers for a 1,600 mm lift pit.
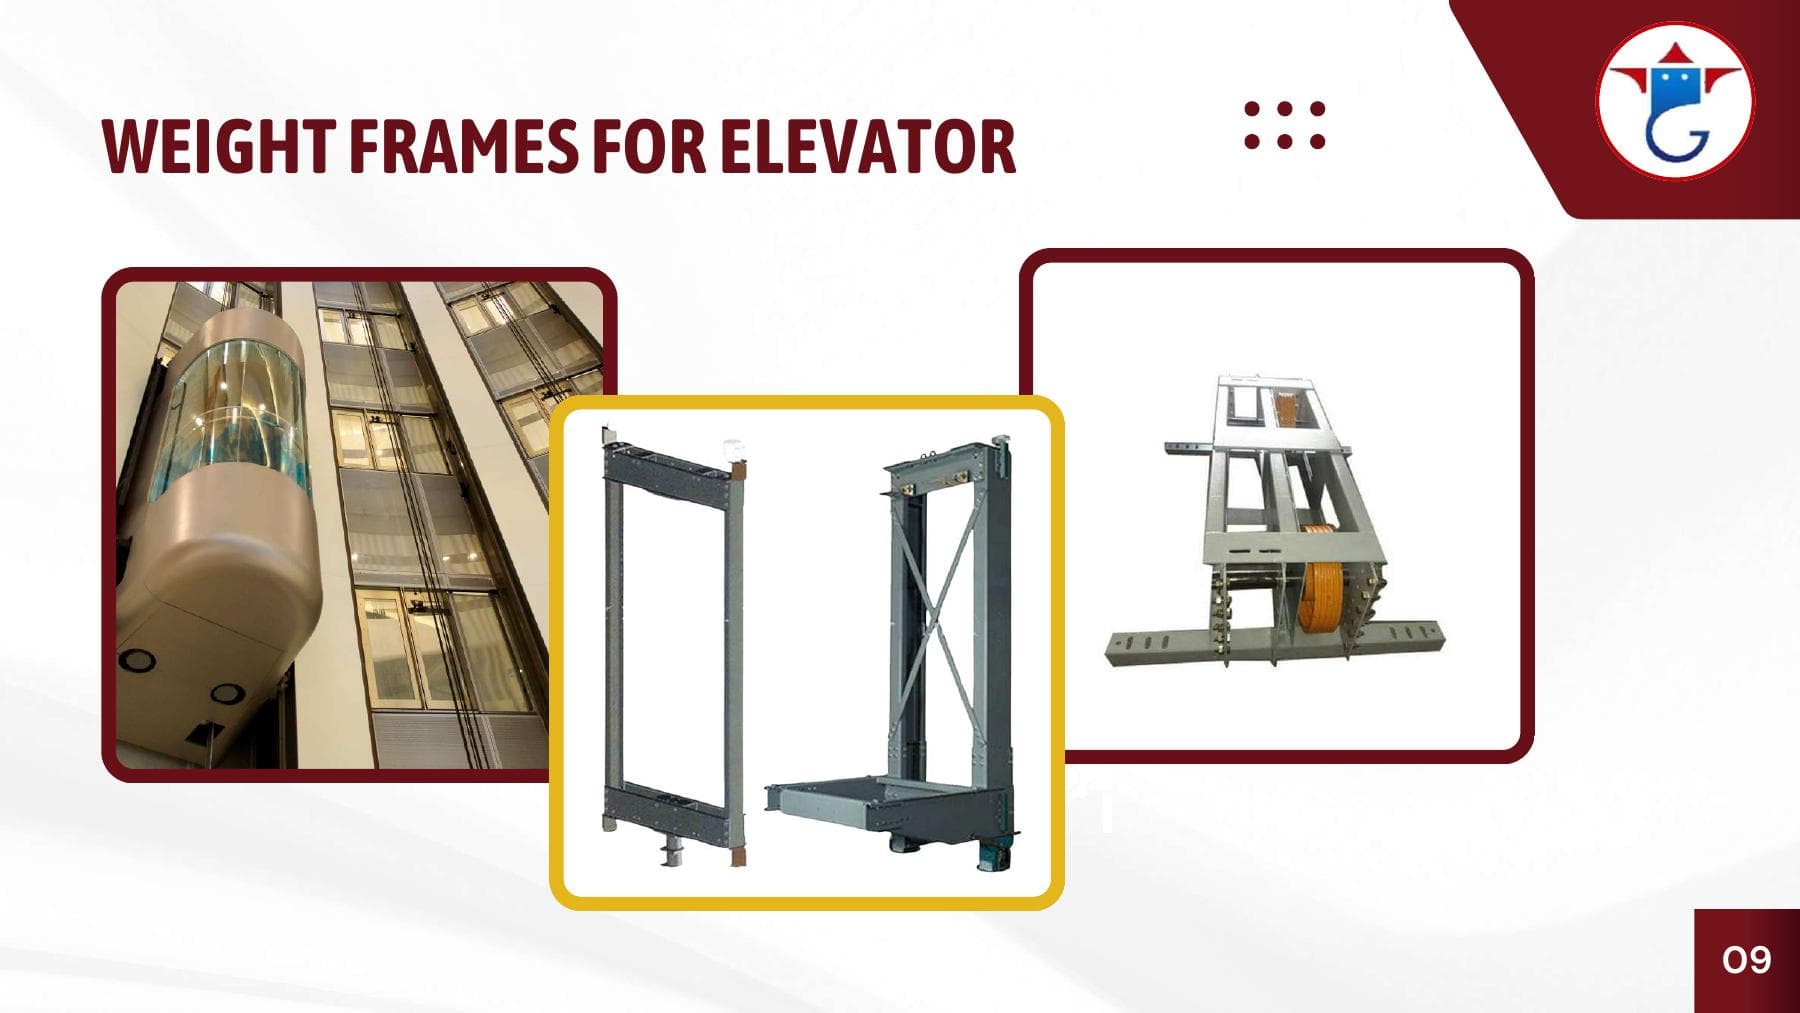
How laser-cut elevator frame sections hold car and counterweight geometry: cut-file rules, hole-to-bend limits, weld distortion and coating checks.
Every article names its reviewer and its sources. Read the RSS feed, or see the engineering team behind the library.