
Key takeaways
- The frame, not the weld bead, decides whether a counterweight runs quietly: a 2 mm diagonal error on a 1,600 mm frame is enough to load the guide shoes unevenly.
- Tack and weld in the fixture on the guide-shoe datums, working from the centre outward in balanced pairs, and hold the frame clamped until it cools below about 150 °C.
- Mask guide-shoe faces and rope-hitch threads before coating; 60–80 µm of powder on a 10.5 mm hole leaves 10.2 mm and a fit that will not assemble.
- Inspect diagonals, guide-face flatness and hitch-hole position on the checking fixture built with the welding fixture, not with a tape on the bench.
- A frame that arrives square and coated still fails if the plate stack is not weighed: a 630 kg lift needs roughly 1,065 kg of counterweight, within about 2% of nominal.
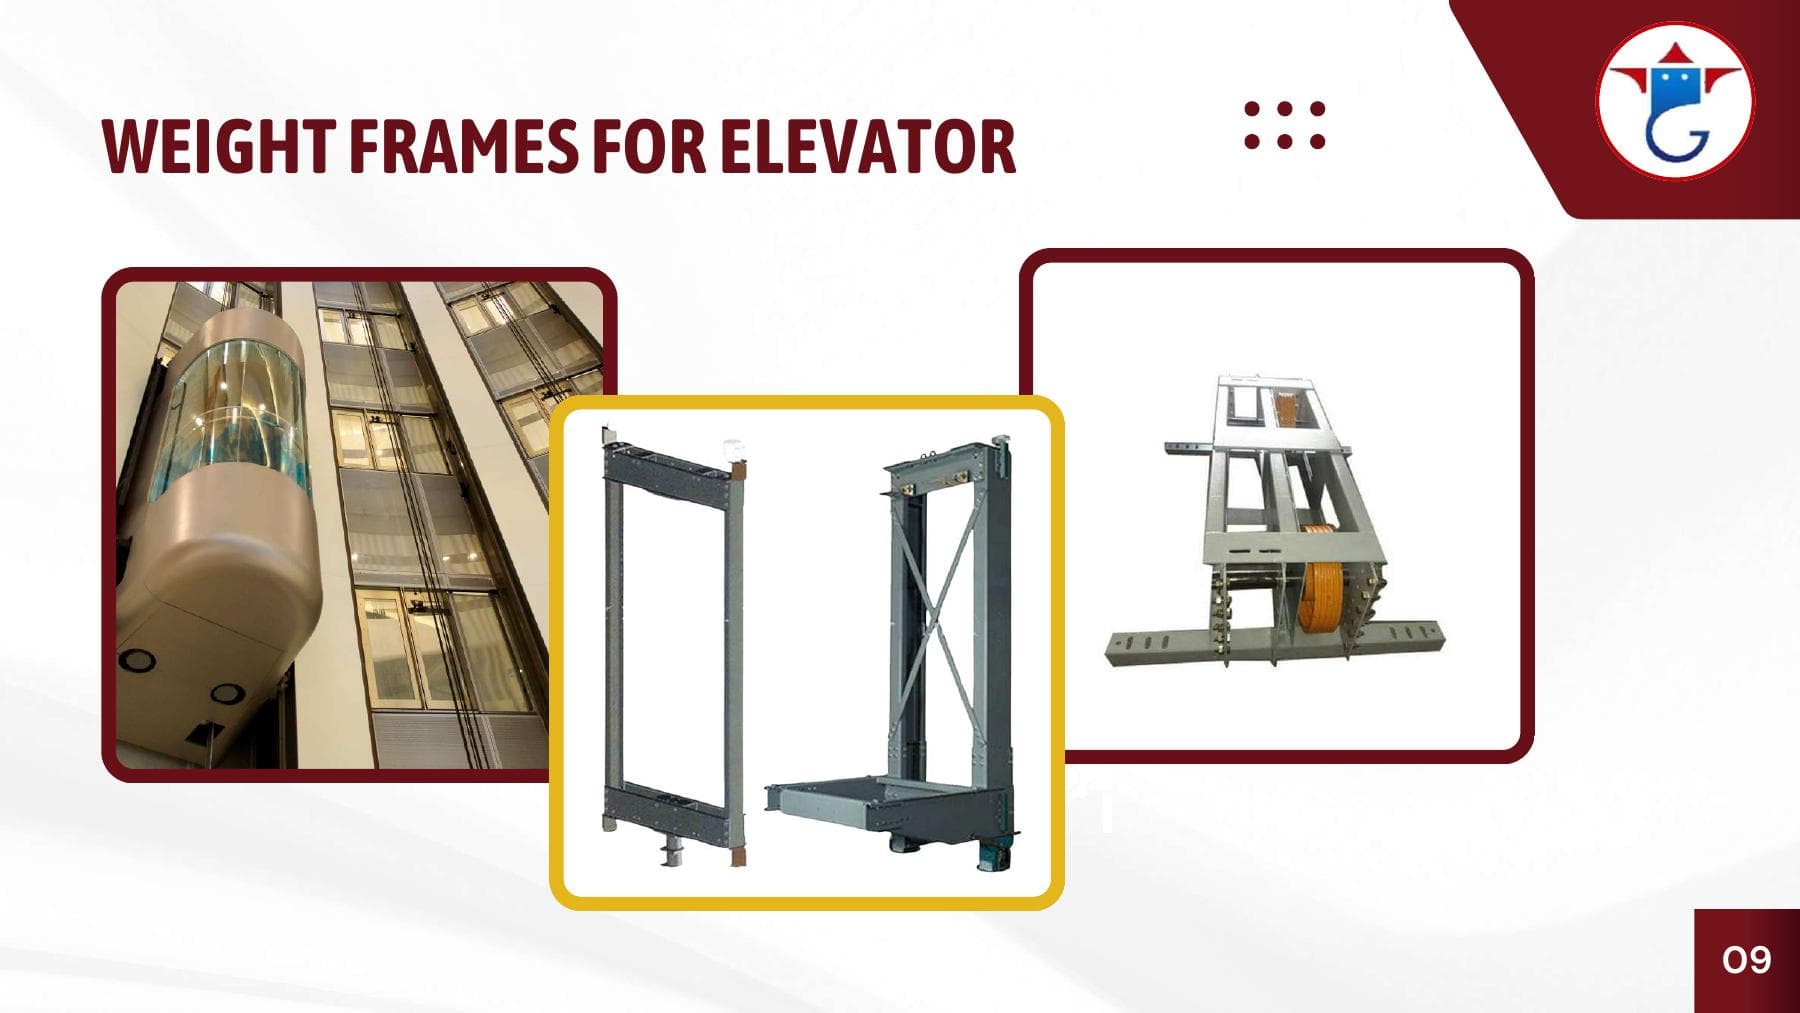
A counterweight frame is a simple weldment with an unforgiving job. It holds a stack of plates that must balance the car, carries the rope hitch, and presents two guide-shoe faces that have to run within a millimetre or two of parallel over a shaft that may be 40 m tall. The weld can pass visual inspection and the frame can still fail at commissioning, because a 2 mm diagonal error on a 1,600 mm frame loads one guide shoe harder than the other and the noise starts on the first trip.
Welded elevator counterweight frames are therefore built around datums and sequence rather than around bead appearance. This guide covers the geometry that decides whether the frame runs quietly, the weld sequence that holds it, the coating and masking detail that stops a fit problem at installation, and the evidence a lift quality team should expect with each lot.
What does the frame actually have to do?
Three jobs, and only one of them is structural. The frame carries the counterweight mass through the rope hitch to the ropes. It holds the plate stack captive so the mass stays where it was balanced. And it locates the guide shoes so the assembly tracks the guide rails without binding.
The mass is calculated, not guessed. Counterweight is normally the car mass plus about 45–50% of the rated load. A 630 kg, eight-person lift with a 750 kg car needs roughly 1,065 kg of counterweight. In steel plate at 25 mm thickness and 1.0 m × 0.3 m per plate, that is about 59 kg per plate, or eighteen plates.
Hold the finished mass within about 2% of nominal, which is ±21 kg on that example, and weigh the assembly rather than trusting the plate count. Coating adds a kilogram or two across a frame this size, and plate thickness tolerance can add more.
Which drawing features decide whether the frame runs quietly?
The table below lists the features worth tolerancing explicitly. A drawing that gives only overall dimensions leaves the toolmaker to choose, and the choice will be made for manufacturing convenience rather than for the shaft.
| Feature | Typical drawing value | Ganesh limit or note | Why it matters on site |
|---|---|---|---|
| Frame sheet thickness | 3–6 mm CRCA or mild steel | 0.8–40 mm range; ±0.5 mm typical on formed features | Thin frames distort more; thick frames load the fixture |
| Diagonal difference | ±1.5 mm on a 1,600 mm frame | Checked on the checking fixture, not with a tape | Skew loads the guide shoes unevenly |
| Guide-shoe face flatness | 0.5 mm over the pad | Faces located in the welding fixture | Shoe clearance is set at installation |
| Guide-face perpendicularity | 0.5 mm per metre | Held by fixture datum, verified on the check fixture | A tilted pad wears one edge of the shoe |
| Rope-hitch hole position | ±0.5 mm | Laser cut and drilled in a fixture | Rope centres must match the sheave plane |
| Fillet weld leg | 4–5 mm | Three CLOOS robotic MIG cells, 30-plus manual stations | Undersized welds on a dynamic load path |
| Weld quality level | ISO 5817 level C or D | Visual and dimensional inspection in process | Sets the acceptance criteria for porosity and undercut |
| Coating | 60–80 µm powder | Seven-tank pretreatment, DFT and cross-hatch adhesion testing | Corrosion in a damp shaft or pit |
| Finished mass | ±2% of nominal | Weighed after coating | Balance and rope tension |
The first row decides how hard the rest is. A 3 mm frame moves more under the same weld heat than a 6 mm frame, so the sequence allowance and the clamping have to match the gauge. If the drawing can accept 5 mm instead of 3 mm on the side channels, the distortion problem gets materially easier and the frame gets heavier by a known amount.
Why does the frame move when the welds cool?
Weld metal shrinks as it solidifies, and the surrounding frame resists that shrinkage. A 4 mm fillet along a 1,500 mm seam deposits a long, thin wedge of metal that contracts in every direction; the corner it sits in is pulled toward the weld, and the diagonals change.
The movement is predictable in direction even when it is not exact in magnitude. Weld one corner completely and the frame pulls to that corner. Weld the two long sides first and the frame bows. Weld from the centre outward in balanced pairs, alternating sides, and the contraction largely cancels.
Four controls hold a frame inside ±1.5 mm on the diagonal. Tack in the fixture on the guide-shoe datums, not on the bench. Weld in a sequence written on the work instruction, not chosen by the operator. Backstep long seams in 200 mm increments. And keep the frame clamped until it has cooled below about 150 °C, because releasing the clamps on hot steel lets the last weld move the geometry you just measured.
How should the weld itself be specified?
Specify the quality level rather than describing the bead. ISO 5817 defines quality levels for imperfections in fusion-welded steel joints, and level C or D is normal for a lift frame depending on whether the joint is on a primary load path. That gives the inspector acceptance criteria for undercut, porosity, spatter and toe profile without an argument about appearance.
Say which welds are structural and which are cosmetic. A cosmetic weld on a visible face needs dressing and a finish that blends; a structural fillet on the hitch plate needs full leg size and no undercut. If the drawing treats them the same, either the cosmetic weld gets more inspection than it needs or the structural weld gets less.
Filler and process matter too. MIG on 3–6 mm mild steel is the standard route, with the gas mix and wire diameter set in the program. On a robotic cell the program is fixed, so the weld is repeatable across the batch; on a manual station the skill of the welder is part of the process, which is why the fixture and the sequence carry more of the quality burden.
How is a car frame different from a counterweight frame?
They look similar in a fabrication shop and are toleranced differently. A counterweight frame carries a dead mass and locates guide shoes; a car frame carries a live load through the sling, the platform and the cab, and its datums include the door sill and the guide rail plane. Door alignment is set on site, but a car frame that arrives twisted makes that alignment a fight.
The practical consequence is that a car frame drawing should state the platform interface and the sill level, not only the overall box. On a sling assembly, the underframe channels and the uprights are welded as one fixture set, because the upright spacing controls where the cab sits relative to the rails. Splitting the frame and the sling across two suppliers reintroduces a tolerance stack at the most visible joint in the lift.
How should a welded frame be inspected?
Inspection starts with datums. Put the frame in the checking fixture on the same guide-shoe locating surfaces the installation will use, then measure the diagonals, the face flatness, the perpendicularity and the hitch-hole position. A frame that passes on the bench and fails in the fixture has told you something useful: the bench was flat, the frame was not.
Record four numbers per lot at minimum: both diagonals, guide-face flatness, hitch-hole position relative to the guide datum, and finished mass. Add the coating record, dry film thickness and the cross-hatch adhesion result. If the frame is welded robotically, keep the program revision with the inspection record, because a program change moves the geometry exactly as a drawing change does.
Then verify the plate stack fit before dispatch. Plates cut to a nominal width and a frame that welded 1 mm narrow will fight at assembly, and the fight happens at the customer's site. A dry assembly of one frame with a representative stack is a cheap test. The welded assembly tolerance guide sets out the general tolerance stack for this kind of fabrication.
What does coating do to a frame that has just been checked?
It adds 60–80 µm everywhere it lands, including the inside of holes and the faces you intended to keep bare. A 10.5 mm clearance hole becomes 10.2 mm, a slot that took a bolt now takes it with effort, and a guide-shoe face that was flat carries a film that compresses unevenly under the bolt.
Mask before coating, not after. Guide-shoe faces, rope-hitch threads and any datum pad should be masked, and the masking method should be in the work instruction. Blasting before coating also removes the weld spatter and heat tint that would otherwise sit under the powder, so the substrate is consistent across the frame rather than only where it was convenient to clean.
Coverage on a frame is uneven by geometry. Internal corners and the inside of the box section receive less powder than the outside face, so measure dry film thickness at named points rather than at the easiest one. The seven-tank pretreatment process is what makes that film adhere; a frame coated over an unprepared surface will fail at the first cross-hatch.
How should a frame be packed for the site?
Frames are awkward loads: long, open, painted on most faces and fitted with two precision pads that must arrive as flat as they left. Ship them in a stillage that supports the frame at the cross members, never at the guide faces, and separate stacked frames with timber that touches the coating rather than the machined pad.
Nest frames of the same part number with the guide faces inboard and the hitch plate protected by a close-fitting board. If two frame sizes travel together, label the stillage by part number and revision, because a mixed load of similar-looking frames is the classic site error. Coated edges take the damage first, so corner protection at the four outer corners of the stack is worth its cost on a long road leg.
Take a photograph of the loaded stillage before the door closes. It settles arguments about transit damage quickly, and it gives the receiving inspector a baseline for what the packing looked like when it was correct.
What does Ganesh Multitech run?
Ganesh Multitech has made sheet metal parts since 1992; five units across Mumbai (Vasai) and Nagpur hold ISO 9001:2015 and ISO 14001:2015 certification and employ more than 200 people. Frames are cut on a 12 kW fibre laser using the full 40 ft × 16 ft bed, formed on a 200 T 5-axis brake with a 4,450 mm bed to 10 mm, and welded on three CLOOS robotic MIG cells or at 30-plus manual MIG, spot and SPM stations. Welding fixtures and checking fixtures are designed and built in the same tool room.
Finishing stays in-house: seven-tank pretreatment, a 16 ft × 16 ft shot blast chamber, an 18 ft × 14 ft electrostatic powder booth, a wet paint booth and a curing oven, with coating thickness and adhesion tested in process. Formed tolerance is ±0.5 mm typical, tighter on critical features by agreement, and first article inspection with PPAP documentation where the programme requires it.
The proof that matters to a lift OEM is the installed base. TKE and Eros Elevators buy elevator frames and parts from us, alongside Mahindra, Mahindra Powerol, Godrej & Boyce, Minda, Gunnebo and Indian Railways across other product lines. The elevator parts route sets out what ships as a finished, coated frame.
When this route does not fit
Four honest limits. We do not machine guide-shoe pads, so a design that specifies a machined face needs that operation planned outside our route, with datums that survive it. We do not cast counterweight plates; frames are fabricated and the plates are bought to mass. A frame that exceeds the 16 ft × 16 ft blast chamber or the 18 ft × 14 ft powder booth needs a coating plan agreed before quotation, sometimes in sections. And several machines are still awaiting confirmed plant assignment, so a quotation names the process, not a unit, until allocation is fixed.
A frame is also the wrong thing to value-engineer below about 3 mm on the side channels without rechecking distortion. The material saving is small against the cost of a fixture that has to fight the weld.
What the lift drawing has to settle
- Frame datum scheme, showing which faces the guide shoes and the rope hitch locate from.
- Diagonal tolerance, and the frame attitude in which it is measured.
- Guide-face flatness and perpendicularity, with the checking method.
- Fillet weld sizes, the ISO 5817 quality level, and the joints that are cosmetic only.
- Coating system, colour, dry film thickness in µm, and the faces to be masked.
- Plate stack mass, plate thickness and the acceptable finished-mass tolerance.
- Annual volume and release pattern, so the fixture and the cell program can be planned.
Send the frame drawing, the stack mass and the volume through the RFQ checklist or straight to request a quote. The fixture review happens before the quote, because the fixture is what holds the diagonal, and the diagonal is what the lift runs on. More frame and sling guidance sits in the elevator components hub and in the counterweight frame overview.
Frequently asked questions
How square does an elevator counterweight frame need to be?
A diagonal tolerance of ±1.5 mm over a 1,600 mm frame is a workable drawing callout, and tighter where the guide shoes are adjustable over a short range. Squareness matters more than absolute size because the guide shoes transfer any skew into the rail, which shows up as noise and uneven shoe wear.
Why do counterweight frames distort after welding?
Every fillet weld shrinks as it solidifies, and the shrinkage is resisted by the frame around it. Welding one corner first pulls that corner in, so the diagonals change by 1–2 mm on a typical frame. Balanced sequences, backstepping and clamping in a fixture that locates on the guide-shoe datums keep the movement inside tolerance.
Should the frame be powder coated or wet painted?
Both are used. Powder gives a tougher, more uniform film at 60–80 µm and suits frames that will be handled in transit. Wet paint is easier where a specific RAL match or a primer system is specified. In either case, mask the guide-shoe faces and any threaded hitch holes before coating.
How much does a counterweight assembly weigh?
The counterweight is normally the car mass plus about 45–50% of the rated load. A 630 kg, eight-person lift with a 750 kg car needs roughly 1,065 kg of counterweight, which is about eighteen 25 mm steel plates at 1.0 m × 0.3 m. The nominal mass should be held within about 2% after coating.
Do you weld the frame and then machine the guide shoe faces?
No. Machined pads sit outside our route, so a design that needs them must plan the machining step and the fixture datums that survive it. Our route holds guide-face position by welding in a fixture built on the same datums used for checking, which avoids machining on most designs.
Sources
Have a counterweight frame drawing?
Send the current revision, plate stack mass, guide shoe interface and annual volume. We will review the fixture, weld sequence and coating masking before quoting the finished frame.
Send a drawing